Multilayered Laminates
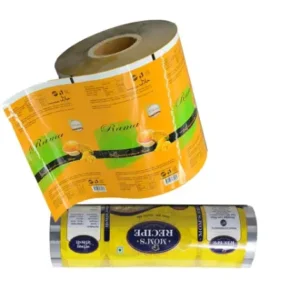
Multilayered Laminates are advanced packaging materials designed to deliver superior strength, durability, and protection for a wide range of products. At Custom Boxes Lab, we specialize in custom multilayered laminates that combine multiple layers of plastic, foil, and polymer films to create high-performance packaging solutions. These laminates are engineered to preserve product freshness, block moisture, oxygen, and external contaminants, making them ideal for food, pharmaceuticals, cosmetics, and industrial goods.
Availability: Made to order
Price: Custom quote – based on your size, quantity, material and print options
How Custom Pricing Works
The $0.10 payment reserves your custom packaging request.
Final pricing depends on:
- Size
- Printing
- Quantity
- Finishing Options
- Material
Our packaging specialist will review your requirements and email you a detailed written quotation – we aim to reply within 24 hours on business days.
Optional: the $0.10 quote reservation fee on each product page is not the product price; where applicable it is adjusted toward your final order.
Send Us Inquiry
Why Choose Custom Boxes Lab?
- Free Professional Design Assistance
- Free Standard Shipping Across the United States
- High-Quality Materials with Premium Printing
- Fully Custom Sizes, Shapes & Finishing Options
- Fast Turnaround with Reliable Delivery
- No Die Plate Charges or Hidden Fees
Description
Multilayered Laminates – Advanced Packaging Solutions for Modern Brands
In today’s highly competitive market, packaging is no longer just a protective shell—it is a critical part of branding, product safety, and customer experience. Multilayered Laminates have emerged as one of the most reliable and advanced packaging materials, offering exceptional strength, barrier protection, and versatility across multiple industries. At Custom Boxes Lab, we bring innovation, engineering expertise, and design precision together to deliver high-performance laminated packaging solutions tailored to modern business needs.
What Makes Multilayered Laminates Essential?
Multilayered laminates are created by combining different layers of materials such as polyethylene (PE), polypropylene (PP), polyester (PET), aluminum foil, and other specialized films. Each layer plays a specific role—whether it is moisture resistance, oxygen blocking, heat sealing, or structural strength.
This layered structure ensures that the packaging performs better than single-material alternatives. It protects products from environmental damage, extends shelf life, and maintains product integrity from manufacturing to end-user delivery.
Custom Multilayered Laminates for Brand-Specific Needs
At Custom Boxes Lab, we understand that every product has unique packaging requirements. That’s why we offer custom multilayered laminates designed according to thickness, barrier level, printing style, and application needs.
Whether you are packaging snacks, frozen food, powders, liquids, or sensitive industrial products, our laminates are engineered to deliver maximum performance. We also ensure that branding elements such as logos, colors, and product information are printed with high-definition clarity, helping your packaging stand out on shelves.
Printed Multilayer Laminate Packaging for Strong Branding
Packaging is a silent salesperson, and visual appeal plays a huge role in customer decision-making. Our printed multilayer laminate packaging combines durability with aesthetic excellence. Using advanced rotogravure and flexographic printing techniques, we create vibrant, sharp, and long-lasting prints that enhance your brand identity.
This makes your packaging not only functional but also visually compelling, increasing product recognition and customer trust in competitive retail environments.
Flexible Multilayer Packaging Films for Versatile Use
Flexibility is a key advantage of modern packaging, especially in industries that require easy handling and storage. Our flexible multilayer packaging films are designed for convenience, adaptability, and high performance. These films can be used for pouches, sachets, wraps, and vacuum packaging applications.
Their lightweight nature reduces shipping costs while maintaining strong protective properties, making them a preferred choice for food and FMCG industries.
High Barrier Laminate Films for Maximum Protection
One of the most important features of multilayered laminates is their barrier capability. Our high barrier laminate films are specifically designed to protect sensitive products from oxygen, moisture, UV light, and odor contamination.
This is especially important for food-grade products, where freshness and hygiene are top priorities. By using advanced barrier technology, we ensure that your products remain safe, fresh, and high-quality for extended periods.
Food Grade Laminated Packaging You Can Trust
Safety is non-negotiable when it comes to food packaging. Our food grade laminated packaging meets strict industry standards to ensure that it is safe for direct food contact. These materials are non-toxic, contamination-free, and designed to preserve taste, aroma, and nutritional value.
From snacks and confectionery to frozen meals and dry foods, our laminated solutions support a wide range of food applications with complete reliability.
Multilayer Plastic Packaging Material for Industrial Use
Beyond food and retail, multilayer laminates are widely used in industrial packaging. Our multilayer plastic packaging material is designed to handle heavy-duty applications, chemical resistance needs, and bulk packaging requirements.
Industries trust our materials for their strength, sealing efficiency, and long-term durability in demanding environments.
Custom Laminated Packaging Pouches for Modern Businesses
Pouches have become one of the most popular packaging formats due to their convenience and aesthetic appeal. We offer custom laminated packaging pouches that are designed with zippers, spouts, and resealable options to improve user experience.
These pouches are ideal for snacks, beverages, cosmetics, supplements, and household products, offering both functionality and premium branding opportunities.
Wholesale Multilayer Laminates for Large-Scale Supply
For businesses requiring bulk packaging solutions, we provide wholesale multilayer laminates at competitive pricing without compromising quality. Our large-scale production capabilities ensure consistency, reliability, and timely delivery for distributors, manufacturers, and retailers.
Durable Barrier Packaging Films for Long-Term Performance
Durability is a key factor in packaging efficiency. Our durable barrier packaging films are designed to withstand handling stress, transportation challenges, and storage conditions while maintaining their protective properties.
This ensures your product remains safe from production to final consumption.
Advanced Multilayer Packaging Solutions by Custom Boxes Lab
At Custom Boxes Lab, we don’t just supply packaging—we engineer complete advanced multilayer packaging solutions. Our approach combines material science, printing technology, and design innovation to deliver packaging that enhances product value and brand identity.
We follow EEAT principles (Experience, Expertise, Authority, and Trustworthiness) by ensuring strict quality control, industry compliance, and customer-focused innovation in every project.
Why Choose Custom Boxes Lab?
- Industry-grade packaging expertise
- Fully customized packaging solutions
- High-quality printing and finishing
- Food-safe and eco-conscious materials
- Bulk and wholesale production capability
- Fast turnaround and reliable delivery
We aim to help businesses elevate their packaging strategy with solutions that not only protect products but also build strong brand recognition in the marketplace.
To get cost-effective packaging boxes without compromising on quality, you can contact us at (469) 649-8706 or email us sales@customboxeslab.com
Frequently Asked Questions
What are multilayered laminates used for?
Multilayered laminates are used for packaging food, pharmaceuticals, cosmetics, and industrial goods due to their strong barrier protection and durability.
Are multilayer laminated packaging materials food-safe?
Yes, our food grade laminated packaging is designed to meet safety standards for direct food contact while preserving freshness and hygiene.
Can I get custom printed multilayer laminates?
Yes, Custom Boxes Lab offers fully customized printed multilayer laminate packaging with branding, colors, and product information.
What makes multilayer films better than single-layer packaging?
They offer superior protection against moisture, oxygen, UV light, and contamination, ensuring longer shelf life and better product safety.
Do you offer wholesale multilayer laminate supply?
Yes, we provide wholesale multilayer laminates for bulk orders with consistent quality and competitive pricing.